Bioactives Manufacturing: How Bioactive Compounds Are Made, Why Production Is Challenging, and How PerMix Solves the Process
Bioactives manufacturing is becoming a major force in food, nutraceutical, pharmaceutical, botanical, and functional ingredient manufacturing. From plant extracts, polyphenols, flavonoids, carotenoids, proteins, peptides, probiotics, enzymes, and botanical actives to specialty wellness ingredients, manufacturers are under growing pressure to produce bioactives with greater precision, better stability, higher bioavailability, and cleaner labels.
At the same time, they must control heat exposure, moisture, oxidation, particle size, homogeneity, and sanitation through every step of production. Those competing demands are exactly why bioactives are one of the most technically demanding sectors in modern process manufacturing.
Scientific research consistently shows that bioactives are often highly sensitive to oxygen, light, pH, heat, and mechanical stress. Encapsulation and gentle drying strategies are increasingly used to preserve activity and improve shelf life and bioavailability.
What Are Bioactives?
Bioactives are compounds that produce a biological effect in the body or in a target system. In commercial manufacturing, the term usually refers to functional ingredients that provide health, nutritional, therapeutic, antimicrobial, antioxidant, anti-inflammatory, digestive, metabolic, or performance-related benefits.
These may come from plants, algae, fermentation, dairy, animal sources, or synthetic and semi-synthetic pathways depending on the application.
Common examples include:
Curcumin
Polyphenols
Anthocyanins
Carotenoids
Collagen peptides
Plant proteins
Botanical extracts
Probiotics
Prebiotics
Essential oils
Omega-rich actives
Specialized nutraceutical compounds
In simple terms, bioactives are valuable because they produce a measurable biological function. The challenge is that many of them are extremely sensitive to processing conditions.
Why Bioactives Matter More Than Ever
The market for bioactives continues to grow because manufacturers across food, beverage, supplements, cosmetics, and pharmaceuticals want products with functional value, cleaner positioning, and scientifically supported performance.
This creates growing demand for:
Concentrated extracts
Fortified powders
Encapsulated actives
Functional ingredient blends
Precision formulated nutritional systems
As this demand increases, manufacturers need equipment that can process delicate materials without degrading them. Preserving performance through industrial processing remains one of the biggest barriers between a promising compound in research and a commercially viable product.
How Bioactives Are Manufactured
Bioactive production is rarely a single step process. Instead, it typically involves a sequence of carefully controlled unit operations.
A typical bioactives manufacturing process includes:
1. Raw Material Handling and Preparation
Production begins with botanical materials, fermentation biomass, powders, oils, proteins, or specialty intermediates.
At this stage manufacturers may require:
Screening
Size reduction
De-lumping
Controlled feeding
Sanitary transfer
Uniform feed characteristics are critical because inconsistent upstream handling can lead to variability in extraction, mixing, drying, and final product performance.
2. Extraction or Isolation
Many bioactives must be separated from plant or biological matrices.
Extraction methods may include:
Water extraction
Ethanol extraction
Solvent extraction
Enzymatic processing
Mechanical disruption
Cold extraction processes
Ultrasound assisted extraction
Modern bioactive production increasingly focuses on greener extraction technologies and higher recovery efficiency from agricultural or botanical raw materials.
3. Concentration and Phase Adjustment
Once extracted, the active fraction is often concentrated or standardized.
At this stage the material may be converted into:
Liquid concentrates
Suspensions
Slurries
Emulsions
Paste intermediates
These intermediate forms determine how the product will be stabilized, dried, or incorporated into downstream formulations.
4. Blending and Standardization
Many bioactives must be blended with carriers, excipients, stabilizers, or functional ingredients.
This stage determines:
Content uniformity
Dispersion quality
Product stability
Target potency
The blending stage is especially critical when the active ingredient is used at very low inclusion rates.
5. Drying
Bioactives are often converted into powders because powders are easier to store, transport, dose, and formulate.
Drying methods may include:
Spray drying
Freeze drying
Vacuum drying
Fluidized bed drying
The challenge is maintaining biological activity while removing moisture.
6. Encapsulation or Microencapsulation
Encapsulation plays a major role in protecting sensitive bioactives.
Encapsulation helps protect compounds from:
Oxygen
Light
Heat
Moisture
pH changes
Premature degradation
Encapsulation technologies may include:
Spray drying
Freeze drying
Nanoencapsulation
Emulsion systems
Biopolymer coating systems
These systems can improve both stability and bioavailability.
7. Final Formulation and Packaging
Once stabilized, bioactives may be incorporated into finished products such as:
Capsules
Tablets
Powdered beverages
Functional foods
Nutraceutical blends
Cosmetic formulations
Pharmaceutical dosage forms
At this stage manufacturers must ensure batch consistency, traceability, and contamination control.
The Biggest Manufacturing Challenges With Bioactives
Bioactive manufacturing presents several significant technical challenges.
Heat Sensitivity
Many bioactives degrade when exposed to high temperatures.
Examples include:
Protein denaturation
Pigment degradation
Loss of volatile compounds
Reduction of biological activity
This is why many processes require low-temperature mixing, controlled residence time, or vacuum drying.
Oxidation
Exposure to oxygen can degrade:
Antioxidants
Plant extracts
Natural pigments
Essential oils
Functional lipids
Processing systems must often include vacuum operation, sealed mixing, or inert gas purging.
Moisture Control
Moisture plays a complicated role in bioactive manufacturing.
Too much moisture can cause:
Clumping
Microbial growth
Chemical degradation
Too little moisture can create:
Poor dispersion
Dust generation
Flow issues
Agglomeration and Powder Flow
Bioactive powders are often extremely fine and cohesive.
Common problems include:
Bridging in hoppers
Electrostatic buildup
Dust generation
Poor discharge behavior
Content Uniformity
Many bioactives are added at extremely low inclusion levels.
Poor mixing can create major potency variation within a batch, which can be unacceptable in regulated industries.
Shear Sensitivity
Some materials require enough energy to disperse properly, but excessive shear can damage their structure or activity.
Balancing mixing intensity with product protection is a critical design factor.
Sanitation and Contamination Control
Bioactive production often occurs in food, nutraceutical, or pharmaceutical environments where sanitation is essential.
Equipment must allow:
Easy cleaning
Product changeovers
CIP or sanitary operation
Controlled product contact surfaces
How Bioactives Are Processed in Real Manufacturing Environments
Different types of bioactives require different processing strategies.
Botanical extracts often involve extraction, concentration, blending with carriers, and spray drying.
Protein and peptide powders typically require gentle blending, liquid addition, controlled agglomeration, and low temperature drying.
Lipid-soluble bioactives often require emulsification, homogenization, carrier incorporation, and encapsulation.
Natural pigments and flavors often require encapsulation to preserve color stability and aroma.
How PerMix Answers the Needs of Bioactives Manufacturers
Bioactive production requires engineered equipment that protects sensitive ingredients while maintaining consistent industrial performance.
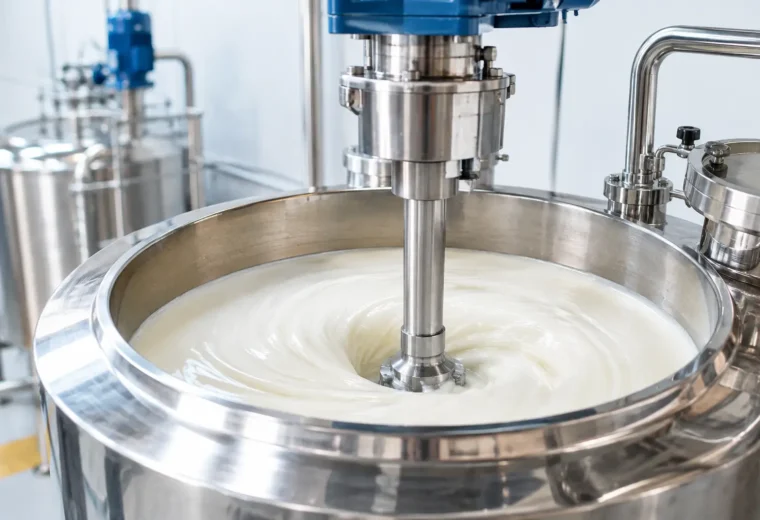
Gentle but Effective Mixing
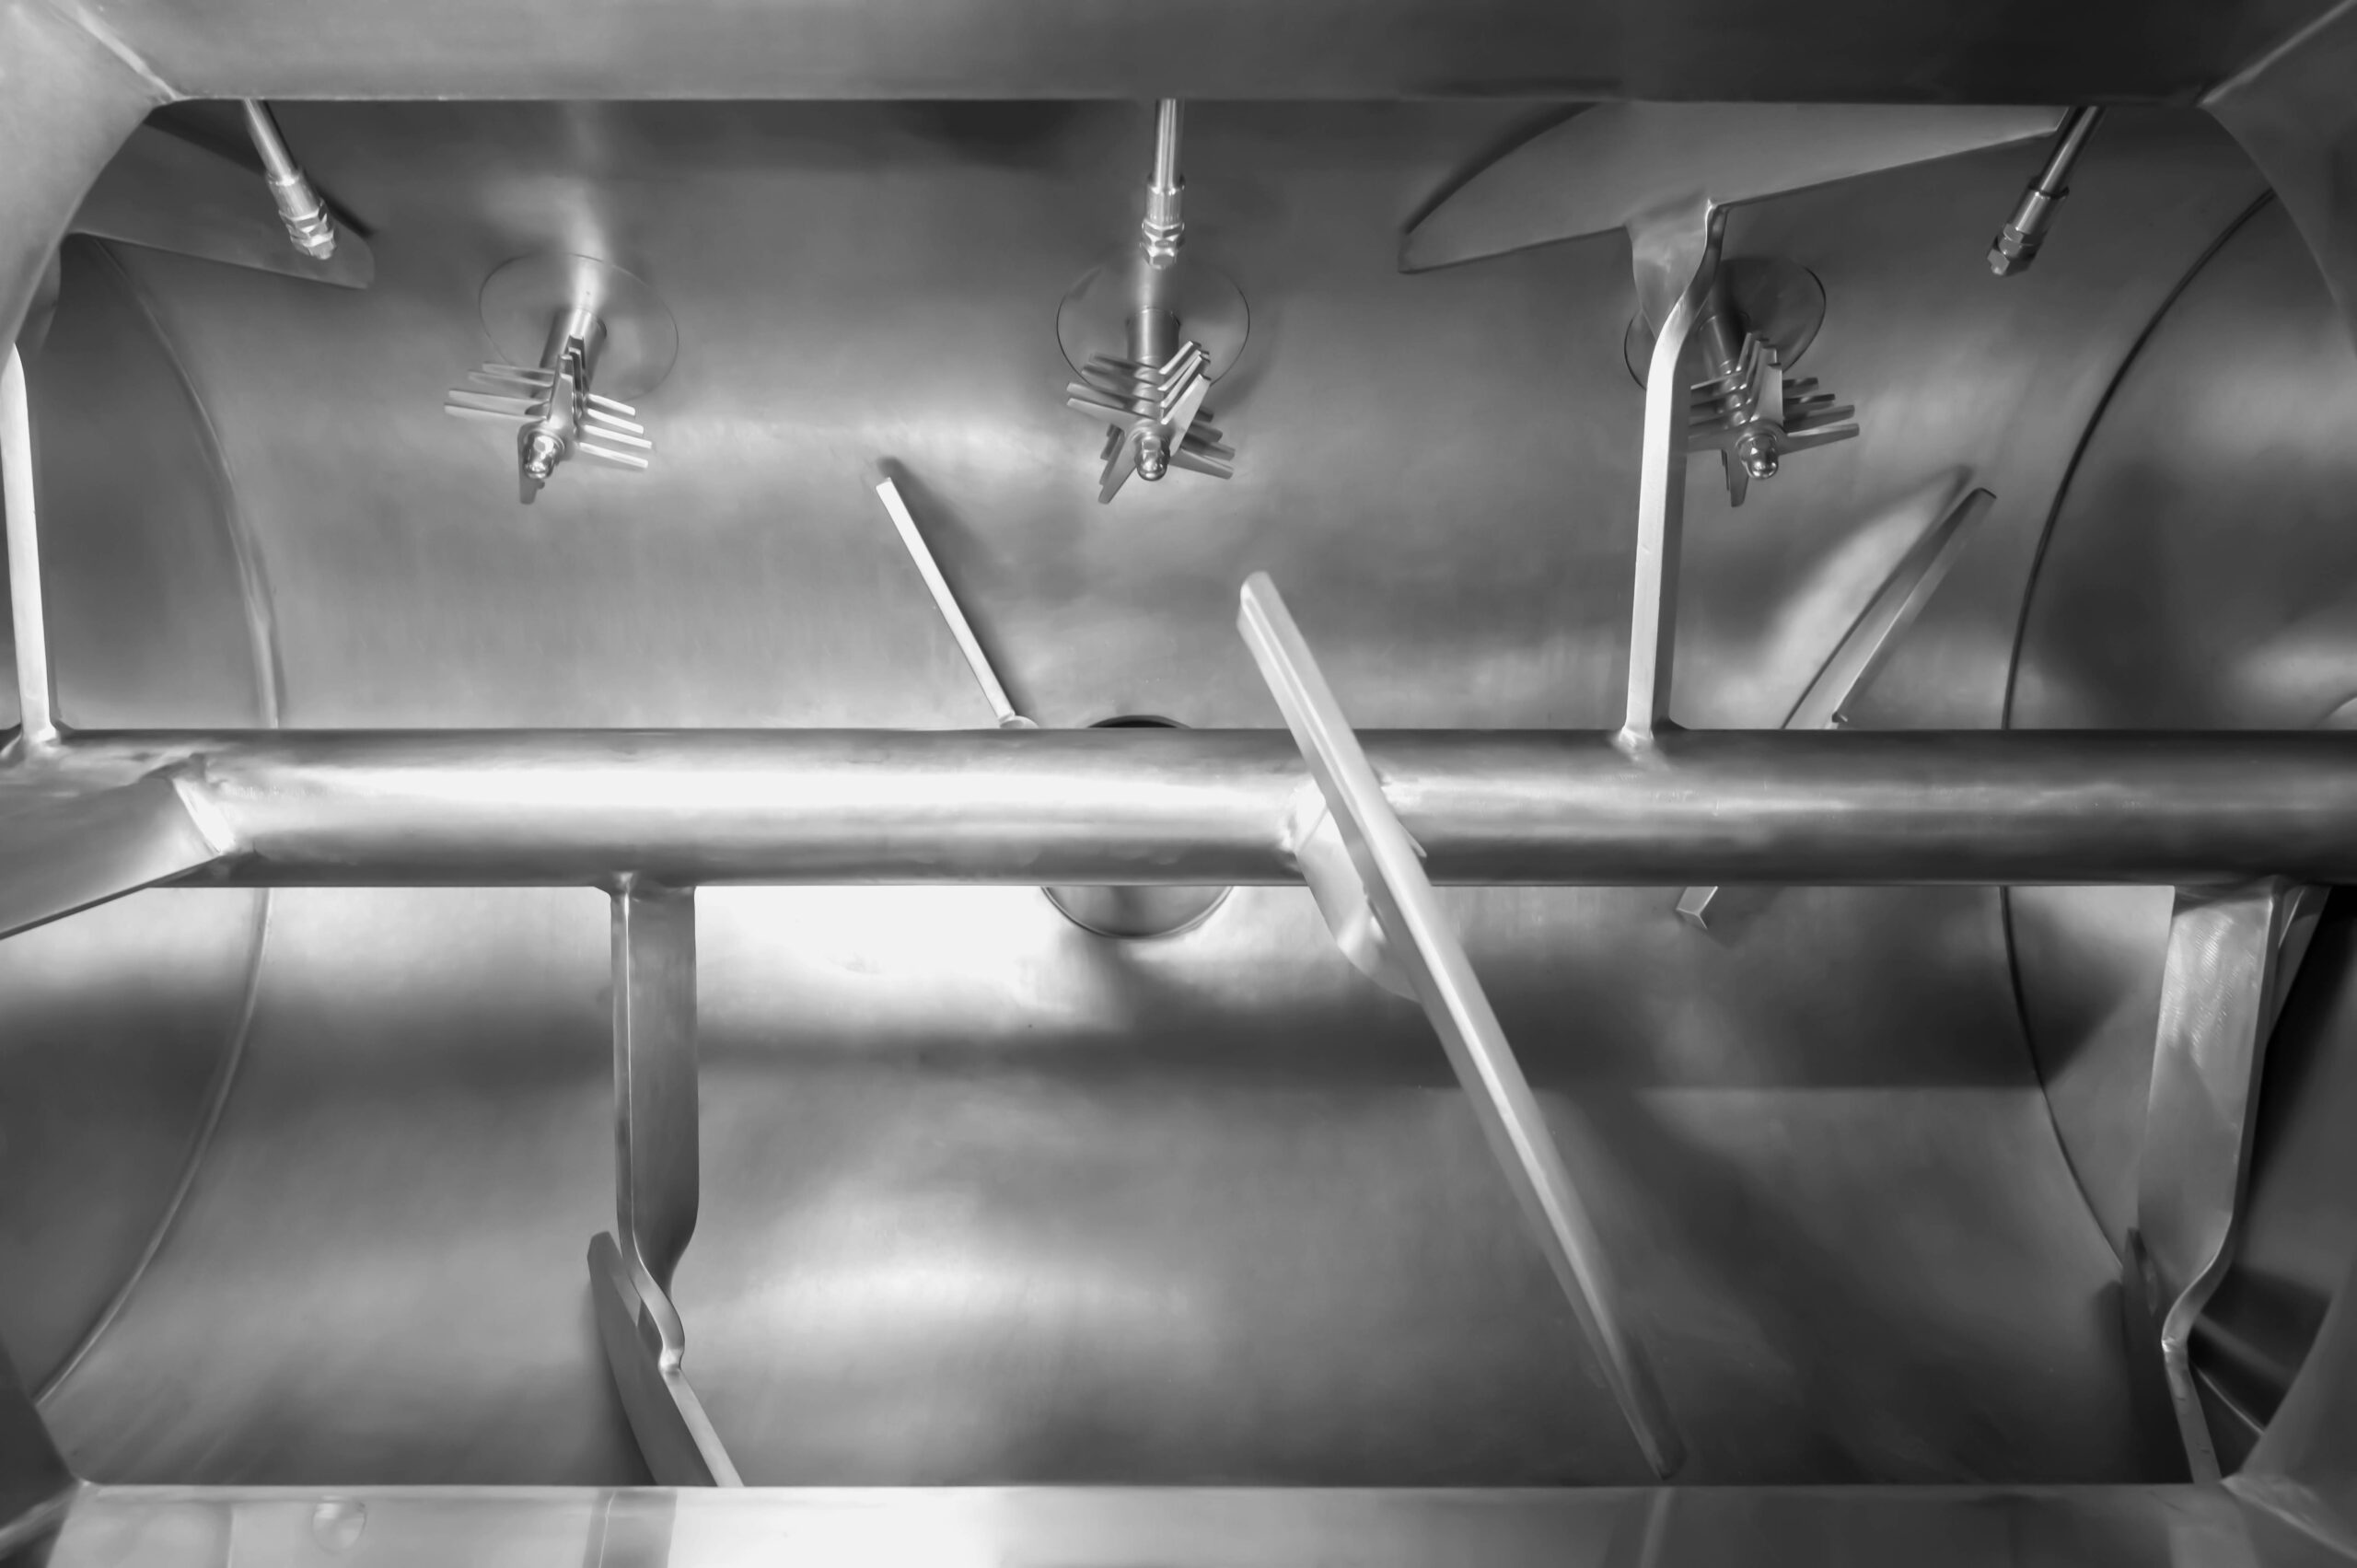
PerMix mixing technologies allow manufacturers to achieve uniform blends while minimizing heat generation and shear damage.
This is critical for delicate materials such as:
Botanical powders
Protein blends
Nutraceutical premixes
Functional ingredients
Liquid Addition Into Powders
Many bioactive formulations require oils, extracts, or active solutions to be sprayed into powder blends.
PerMix systems can integrate:
Spray nozzles
Metered liquid dosing
Intensifier tools
Choppers
This ensures uniform coating and prevents clumping.
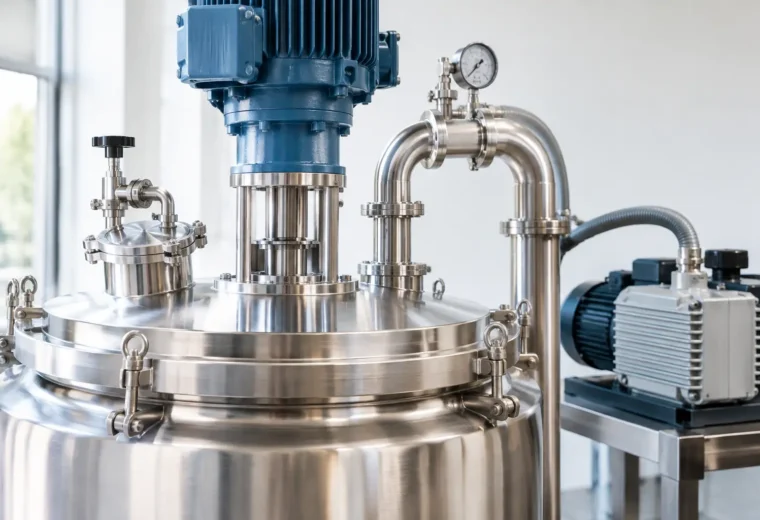
Vacuum Mixing and Drying
Vacuum operation offers significant advantages for heat sensitive or oxygen sensitive materials.
Vacuum processing allows:
Lower temperature drying
Reduced oxidation
Improved solvent removal
Improved product protection
This is particularly useful for botanical extracts, nutraceutical powders, peptides, and specialty chemicals.
Temperature Control
Jacketed mixing systems allow precise temperature management during processing.
This helps prevent hotspots, protect sensitive compounds, and maintain batch consistency.
Support for Encapsulation Processes
PerMix equipment supports upstream stages of encapsulation processes including:
Pre-blending
Carrier preparation
Emulsion mixing
Feed preparation for drying systems
Hygienic Design
PerMix equipment can be designed with sanitary construction, polished surfaces, and cleanable geometries to support food, nutraceutical, and pharmaceutical production.
Scalable Manufacturing
Processes that work at laboratory scale often behave differently at production scale.
PerMix supports scale-up strategies that help maintain product performance from R&D to commercial manufacturing.
Why Equipment Selection Matters in Bioactives Processing
In conventional powder blending, poor equipment may simply reduce efficiency.
In bioactives manufacturing, poor equipment can destroy product value while the finished powder still appears acceptable.
Potential problems include:
Reduced potency
Oxidation damage
Poor dispersion
Non-uniform active distribution
Loss of aroma or color
Shortened shelf life
This is why the design of mixing, drying, vacuum, and liquid-addition systems is critical to maintaining product integrity.
PerMix Solutions for Bioactives Manufacturing
Bioactives manufacturing requires a careful balance between protecting fragile compounds and maintaining a reliable industrial process.
PerMix provides mixing, vacuum processing, drying, and powder handling technologies that allow manufacturers to maintain the performance of sensitive bioactive ingredients while achieving consistent production results.
Whether the process requires powder blending, liquid addition, vacuum drying, temperature control, or sanitary operation, PerMix equipment is engineered to support the unique demands of bioactive ingredient manufacturing.
In bioactives processing, the molecules may be small, but the consequences of poor processing are enormous. Precision equipment and well-engineered processes are essential to protecting the value of these high-performance ingredients.