A batch can look fully mixed and still contain enough air to create a costly downstream problem. Pinholes in coatings, unstable density in filled products, poor heat transfer, inaccurate fill weights, and weak adhesive bonds often begin with the same question: can vacuum remove entrained air? In many applications, yes – but only when vacuum is matched to the material rheology, vessel design, mixer action, and the way air entered the product.
Vacuum is not a universal correction for poor processing. It is a controlled deaeration tool. Applied correctly, it can remove dispersed bubbles and headspace gases efficiently while protecting product consistency. Applied without regard for foam behavior, viscosity, vapor pressure, or agitation, it can slow the batch, pull off volatile components, or create a vessel overflow.
Can Vacuum Remove Entrained Air Effectively?
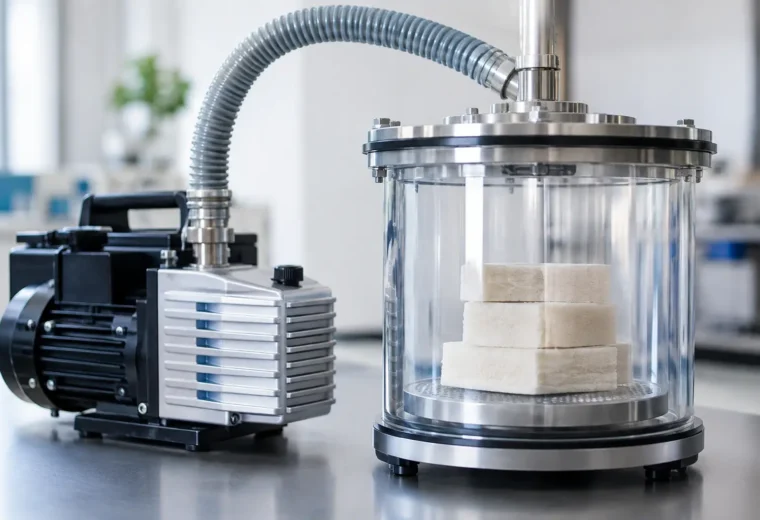
Vacuum removes entrained air by reducing the pressure above the product. As pressure falls, trapped gas bubbles expand. Larger bubbles rise more readily through the material and break at the product surface, where the vacuum system evacuates the released gas.
The mechanism is straightforward, but the process result depends on bubble mobility. In a low-viscosity liquid, air bubbles can rise and disengage quickly. In a high-viscosity paste, sealant, polymer compound, battery slurry, or filled resin, bubbles may remain trapped within the material structure. Vacuum can expand them, but expansion alone does not guarantee removal. The process may require controlled mixing, wall scraping, heating, or a longer hold period to expose those bubbles to the free surface.
The practical answer is therefore: vacuum can remove entrained air, often very effectively, but it must be designed as part of the process rather than added as an afterthought.
Entrained Air Is Not the Same as Dissolved Gas
Process teams sometimes use the terms interchangeably, yet they behave differently under vacuum. Entrained air exists as visible or microscopic bubbles dispersed through a liquid, slurry, paste, or viscous mass. It is commonly introduced during powder charging, liquid addition, recirculation, pumping, high-speed agitation, or inadequate vessel filling.
Dissolved gas is molecularly dispersed in the liquid phase. Reducing pressure can encourage dissolved gas to come out of solution, creating new bubbles that then need time and a path to escape. This is why a product may appear to foam more aggressively after vacuum is applied. The vacuum is not adding air. It is exposing gas already present in the formulation.
For some products, especially solvent-containing systems, the process must distinguish between removing air and removing volatile ingredients. A deep vacuum at elevated temperature may strip solvent, fragrance, water, or reactive monomers along with air. That can change viscosity, solids content, odor profile, reaction performance, and final product specifications.
What Determines Whether Deaeration Will Work?
The most important variable is viscosity. Low-viscosity materials release air with relatively little assistance. As viscosity rises, bubble rise velocity drops sharply, and the product may require more process energy or more residence time under vacuum. A material that deaerates in minutes at 5,000 cP may require substantially different equipment and operating conditions at 500,000 cP.
Bubble size also matters. Large bubbles are comparatively easy to remove. Fine bubbles, particularly those stabilized by surfactants, binders, proteins, pigments, or particulate networks, can persist much longer. In these systems, controlled folding and surface renewal may be more valuable than high-speed dispersion during the deaeration stage.
Temperature affects both viscosity and vapor pressure. Moderate heating can reduce viscosity and improve bubble movement, but it also increases the risk of boiling or volatile loss under vacuum. The operating temperature and vacuum level must be evaluated together, not selected independently.
Formulation chemistry can be equally decisive. Foaming products may rapidly expand when vacuum is applied. A vessel needs sufficient freeboard, and the vacuum ramp should be controlled to avoid product carryover into piping, condensers, filters, or vacuum pumps. Antifoam may help in some formulations, but it is not always acceptable in regulated, high-purity, optical, food, or coating applications.
Mixer Design Has a Direct Effect on Air Removal
A vacuum vessel alone is not necessarily a deaeration system. The mixer must move material in a way that releases trapped air without continuously folding more air back into the batch.
For free-flowing liquids and emulsions, a vacuum-rated high shear mixer or homogenizer may provide the dispersion and circulation needed before a lower-intensity deaeration stage. The operating sequence matters. High shear is useful for wetting powders, breaking agglomerates, and creating an emulsion, but excessive speed under vacuum can increase foam or make deaeration less efficient.
For high-viscosity products, multi-shaft mixers, double planetary mixers, and sigma mixers can provide the necessary bulk movement. Planetary blades sweep the vessel volume and continuously expose fresh material to the surface. Wall scrapers prevent stagnant material from remaining on the vessel wall, where air may stay entrapped. In dense formulations, this controlled movement is often the difference between acceptable deaeration and a batch that remains porous after extended vacuum holding.
Vacuum deaerators are particularly effective when the product can be spread into a thin film or exposed across a large surface area under reduced pressure. This approach reduces the distance bubbles must travel before release. It can be well suited to coatings, adhesives, resins, slurries, and other products where consistent air removal is required before filling, coating, casting, or downstream processing.
The Risk of Applying Vacuum Too Quickly
A deeper vacuum is not always a better vacuum. Pulling pressure down too quickly can cause a foaming material to expand several times its original volume. The immediate result may be lost production time, contamination of the vacuum line, and material carryover. More seriously, an uncontrolled event can create cleaning, maintenance, and quality issues that extend well beyond one batch.
A staged vacuum profile is usually more reliable. The process may begin with a partial vacuum to initiate bubble growth gradually, followed by controlled agitation and a deeper vacuum once the bulk foam subsides. The proper profile depends on material behavior, vessel freeboard, batch size, and the capacity of the vacuum system.
Vacuum system sizing also deserves attention. The pump must remove air and vapor at a rate that supports the process, while the piping, condensers, filters, and separators must protect the equipment. A system designed only around ultimate vacuum level can underperform if it cannot handle the actual vapor load produced by the batch.
How to Specify a Vacuum Deaeration Process
A productive equipment discussion begins with process data, not a mixer model number. The material’s viscosity profile, density, solids loading, temperature limits, volatility, foam tendency, particle size, and sensitivity to shear all influence the recommended configuration.
The production objective should be equally clear. Some operations need to eliminate visible bubbles before packaging. Others need extremely low void content because small defects compromise electrical insulation, optical clarity, coating appearance, laminate strength, or dispensing accuracy. These are different specifications and may require different methods of validation.
Useful acceptance criteria can include final density, void percentage, bubble size, coating defect rate, product appearance, fill-weight repeatability, or downstream reject rate. A vacuum level alone is not a meaningful quality target. The target should be the measurable product result that vacuum processing must achieve.
Pilot testing is often the fastest route to a reliable specification. It confirms whether the material releases air under practical conditions, identifies the right mixing and vacuum sequence, and reveals whether heating or staged pressure reduction is necessary. It also helps quantify batch-cycle time, which is essential when deaeration becomes a production bottleneck.
When Vacuum Is Not the Entire Answer
If air is continually introduced upstream, vacuum treatment at the end of the batch may only treat the symptom. Powder induction systems that draw excessive air, leaking pump seals, poorly designed recirculation loops, vortexing in open vessels, and uncontrolled ingredient addition can all load a formulation with gas before it reaches the vacuum stage.
The better approach is to reduce air incorporation at the source and use vacuum to remove the remaining entrained gas. This may involve submerged liquid addition, low-aeration powder induction, improved feed rates, correct impeller submergence, or pump selection suited to the material. The result is a shorter deaeration cycle, less foam risk, and greater batch repeatability.
PerMix engineers vacuum mixing and deaeration systems around these full-process variables, including material handling, agitation, thermal control, vacuum performance, discharge, and cleaning requirements. The objective is not simply to pull vacuum. It is to produce a stable, repeatable product at the required production rate.
Before selecting equipment, run the material under representative conditions and define the defect that air is causing. That evidence turns vacuum deaeration from a general capability into a controlled process solution that protects quality on every batch.