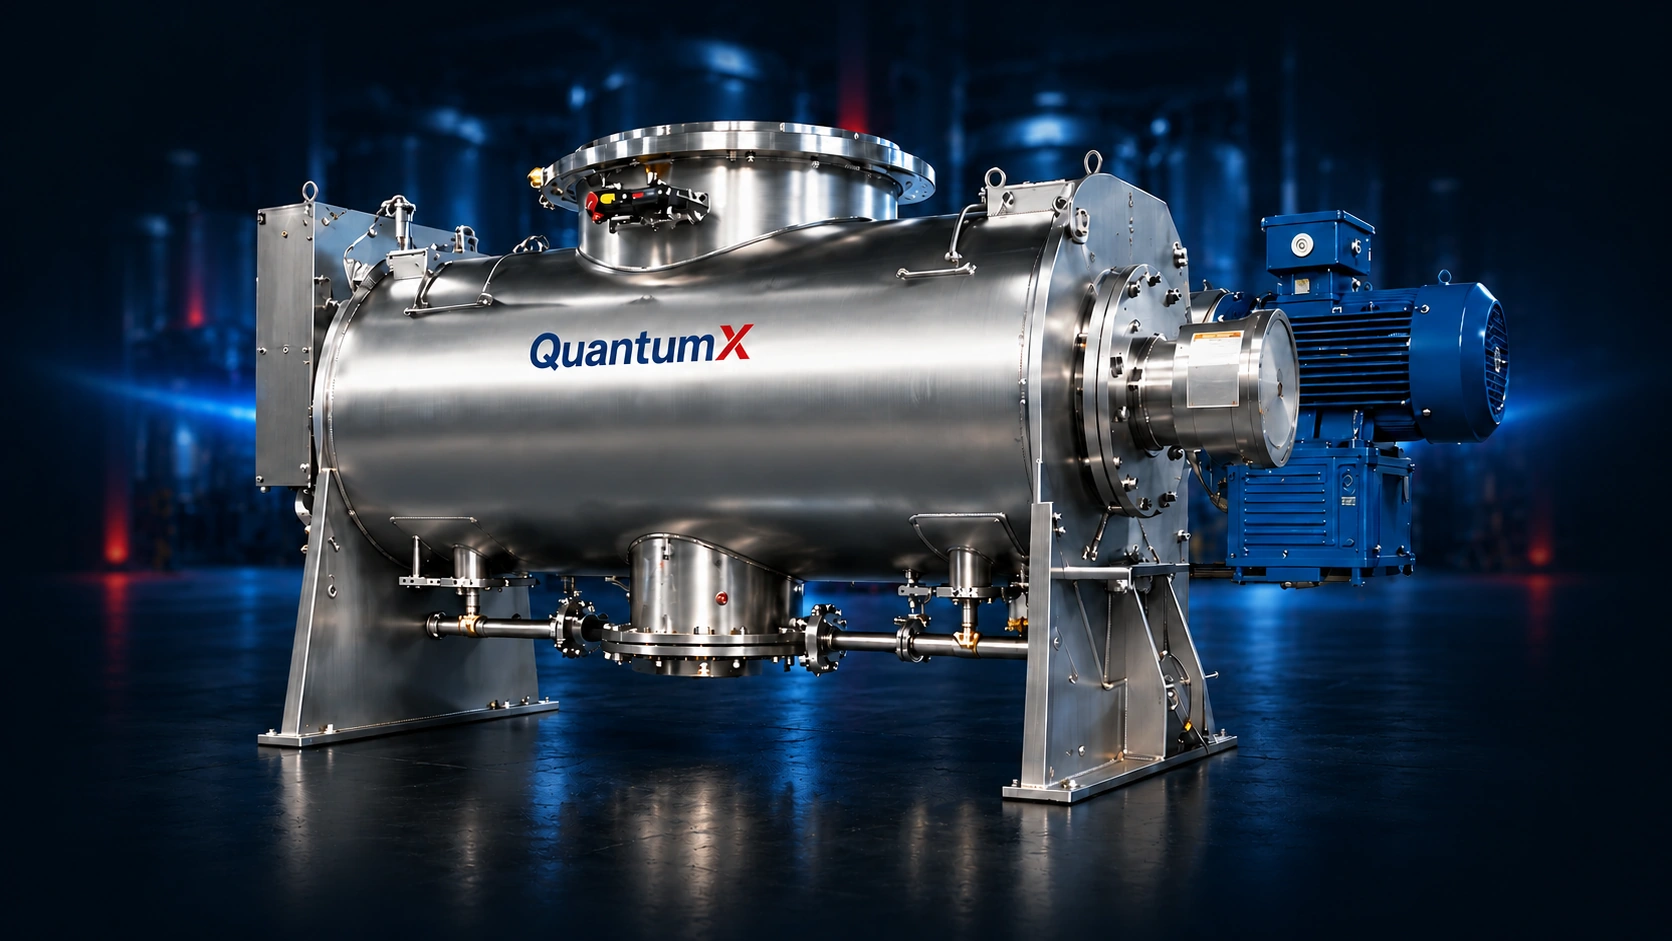
QuantumX horizontal intensive mixer for fluidized-zone powder processing

RAPID PARTICLE EXCHANGE CONTROLLED MECHANICAL FLUIDIZATION SHORT BATCH CYCLES

QuantumX Fluidized-Zone Mixers

Fluidized-Zone Mixers Engineered for Speed, Uniformity and Product Control

QuantumX fluidized-zone mixers use engineered paddle systems to lift, separate and redistribute powders through a mechanically fluidized mixing region.

In the primary twin-shaft configuration, two counter-rotating paddle shafts operate inside a W-shaped vessel. The paddles sweep the lower troughs and project material toward the open region between the shafts, creating overlapping active zones where particles move rapidly and exchange throughout the batch.

Compare Fluidized Zone, Paddle, Ribbon & Plough Mixers

Overview

What Is a Fluidized-Zone Mixer?

A fluidized-zone mixer is a batch mixer designed to create rapid particle mobility through mechanical agitation rather than through the process air used in a pneumatic fluid-bed system.

The primary QuantumX configuration uses:

  • Two parallel horizontal shafts
  • Counter-rotating paddle tools
  • A W-shaped or twin-trough vessel
  • Engineered paddle angles
  • Overlapping product trajectories
  • Controlled working fill
  • Open space above and between the shafts

As the shafts rotate, the paddles lift material from the lower portions of the vessel and project it toward the central mixing region.

The material is temporarily separated and mobilized, creating a lower-density, highly active zone where particles can exchange position rapidly.

The result is not literal zero gravity.

It is a mechanically induced state of reduced bulk contact and increased particle mobility.

Commercial twin-shaft fluidized-zone mixers use counter-rotating paddles to sweep the troughs and create a central region where particles can move and intermix with less friction than in a densely packed powder bed.

Key capabilities

Key Capabilities

Legacy PerMix technical literature describes the twin-shaft system as two counter-rotating paddle shafts in a W-shaped trough, with paddles sweeping the lower vessel and lifting material into a fluidized zone between the shafts.

This mixing principle can provide:

  1. Rapid powder blending
  2. Short batch cycles
  3. Distribution of low-percentage ingredients
  4. Mixing of ingredients with different particle sizes and bulk densities
  5. Controlled liquid addition
  6. Particle coating
  7. Gentle handling of selected fragile products
  8. Reduced frictional heat for suitable formulations
  9. Rapid full-length discharge
  10. Integration with weighing, feeding and packaging
  11. Application-specific vacuum, pressure, ATEX and containment configurations

Mechanical fluidization

Mechanical Fluidization Is Not Pneumatic Fluidization

No Process Air Is Required to Create the Principal Mixing Action

The term “fluidized zone” can be confused with fluid-bed dryers, coolers and processors that suspend particles using a large volume of process air.

A QuantumX fluidized-zone mixer creates its principal mixing action mechanically.

The paddles provide the energy required to:

  • Lift the material
  • Separate particles
  • Exchange material between troughs
  • Move ingredients toward and away from the center
  • Renew product exposure to liquid sprays
  • Circulate the complete batch

Compressed air or process gas may still be used for:

  • Seal purging
  • Nitrogen inerting
  • Dust-filter cleaning
  • Instrumentation
  • Pneumatic conveying
  • Product-specific processing

But it is not normally the primary mechanism that creates the mixing zone.

Why This Distinction Matters

Mechanical fluidization can provide:

  • Compact equipment
  • Batch control
  • Rapid start and stop
  • No large process-air system for the mixing action
  • Reduced downstream air separation
  • Easier containment than an open pneumatic-fluidization process
  • Direct integration with load cells and batch controls

Shaft architecture

Twin-Shaft and Single-Shaft Fluidized-Zone Mixing

Twin-Shaft Fluidized-Zone MixingTwo Counter-Rotating Shafts Create Overlapping Active Zones

The twin-shaft design is the principal architecture for high-performance fluidized-zone mixing.

Each shaft carries a series of paddles arranged at controlled angles.

During operation:

  • The paddles sweep the lower trough regions.
  • Material is lifted from both sides.
  • Product is directed toward the center and upper mixing region.
  • The two shaft systems create overlapping trajectories.
  • Particles separate, exchange and recombine.
  • Material returns toward the lower troughs.
  • The cycle repeats throughout the batch.

The interaction between both shafts creates stronger cross-vessel exchange than a conventional single-shaft mixer.

Potential Advantages

  • Rapid total-batch circulation
  • Strong exchange between materials of different densities
  • Short blend cycles
  • High production throughput
  • Broad ingredient distribution
  • Effective spray exposure
  • Reduced persistent end zones
  • Controlled handling of fragile particles
  • Rapid discharge through large bottom doors

Strongest Preliminary Fit

Twin-shaft systems are often considered when:

  • Production batches are large
  • Cycle time is critical
  • Density differences are significant
  • Minor ingredients must distribute rapidly
  • Liquid must be applied uniformly
  • High throughput is required
  • A full-length discharge system is valuable
  • Product integrity must be balanced with rapid blending

Single-Shaft Fluidized-Zone MixingA Simpler Architecture for Selected Applications

A single-shaft fluidized-zone mixer can be evaluated for applications that do not require the full interaction of two counter-rotating shafts.

Potential benefits can include:

  • Reduced mechanical complexity
  • Lower capital cost
  • Simpler drive arrangement
  • Fewer shaft seals
  • Easier access
  • Lower maintenance requirements
  • Suitable performance for selected free-flowing powders

Potential limitations can include:

  • Less cross-vessel interaction
  • Reduced overlapping fluidization
  • Longer circulation path
  • Lower performance with difficult density differences
  • Reduced liquid-distribution intensity
  • Less production flexibility for demanding formulas

Preliminary Selection Direction

Choose a single-shaft system when:

  • The formulation is relatively simple
  • The product flows well
  • Batch size is moderate
  • Liquid addition is limited
  • Cycle-time requirements are less aggressive
  • Simplicity is a priority

Choose a twin-shaft system when:

  • Maximum particle exchange is required
  • The batch contains significant density or particle-size differences
  • Liquid addition or coating is important
  • The batch is larger
  • Throughput is critical
  • The material is more difficult to mix

Final selection remains product- and process-specific.

Geometry

The Geometry That Determines Fluidized-Zone Performance

Engineering VariableWhat It InfluencesWhy It Matters
Paddle widthProduct capture, lift and active surface areaToo little width can weaken circulation; excessive width can increase torque and product impact.
Paddle face angleDirection of material projectionThe angle determines whether material moves upward, inward, outward or axially.
Paddle profileProduct release and local shearThe leading edge and curvature affect whether particles lift cleanly or compact ahead of the tool.
Paddle spacingFrequency of engagement along each shaftPoor spacing can create weak end zones or excessive local intensity.
Paddle overlapExchange between neighboring active zonesCorrect overlap helps prevent isolated circulation cells.
Shaft center distanceInteraction between the two paddle systemsShaft spacing affects the size and intensity of the central fluidized region.
Shaft rotational directionCentral exchange and trough circulationCounter-rotation must direct product toward the intended mixing zone.
Shaft synchronizationStability of the overlapping trajectoriesControlled phase relationship helps maintain repeatable product movement.
Rotational speedProduct lift, fluidization and impactSpeed must be high enough to mobilize the batch without causing unnecessary damage or heat.
Total active paddle areaQuantity of material influenced per revolutionSurface area must be sufficient for rapid movement without creating excessive drag.
Paddle-to-vessel clearanceBottom sweep and residual hold-upExcessive clearance can leave slow-moving material; insufficient clearance creates contact risk.
Paddle-to-paddle clearanceInteraction between shaft systemsThe tools must create overlapping zones without mechanical interference.
Vessel geometryProduct trajectories and dischargeThe W-shaped trough must support both lower sweep and central exchange.
Working fillAbility to create the fluidized zoneToo little product weakens exchange; too much product suppresses particle separation.
HeadspaceAvailable room for particle liftThe batch requires sufficient open volume for the intended mechanically fluidized action.
Product propertiesTorque, lift, circulation and damage riskDensity, cohesion, fragility, moisture and shape directly affect performance.

Process engineering

01Topic

Paddle Angle Is Not a Standard Catalog Detail

The paddle angle determines where the product moves after it is captured.

A paddle may be designed to:

Lift material upwardMove product toward the vessel centerMove product toward an endReturn material toward the lower troughSupport discharge-zone circulationCreate axial exchangeExpose product to a spray zone

If every paddle is positioned without regard to the overall circulation pattern, the mixer may create visible turbulence while leaving weakly exchanged regions.

QuantumX evaluates the entire paddle sequence.

The objective is to create:

Complete trough sweepEnd-to-center exchangeShaft-to-shaft exchangeStable central particle mobilityControlled spray exposurePredictable discharge

02Topic

Counter-Rotation and Shaft Synchronization

The twin shafts must operate as a coordinated pair.

Important considerations include:

Direction of rotationRelative shaft speedPhase relationshipGearbox arrangementChain or timing systemIndependent drivesTorque distributionShaft deflectionPaddle clearancesOverload behaviorEmergency stopping

Potential drive architectures include:

One motor with mechanical synchronizationOne motor with dual gearboxesDual synchronized drivesIndependent variable-frequency drives with electronic coordination

Single Mechanical Drive

Potential advantages:

Inherent mechanical synchronizationSimpler controlsOne primary motor

Potential considerations:

Chain or timing-component maintenanceShared load pathMechanical access

Dual Independent Drives

Potential advantages:

Flexible shaft-speed controlIndependent motor monitoringEasier distribution of high loadsApplication-specific speed strategies

Potential considerations:

Electronic synchronizationMore complex controlShaft-phase managementFault handling

03Topic

Working Fill and Headspace

Fluidized-Zone Mixing Requires the Correct Product Level

The mixer needs enough material for the paddles to capture and exchange the batch.

It also needs enough open volume above the product for particles to lift and separate.

Underfilling Can Cause

Incomplete paddle engagementWeak shaft-to-shaft exchangeProduct remaining in isolated trough regionsInconsistent liquid exposureLonger mixing timeIncreased particle impact

Overfilling Can Cause

Suppressed particle separationReduced central fluidizationIncreased torqueProduct compactionPoor spray distributionLonger mixing timeHigher motor load

The correct working fill depends on:

Vessel geometryShaft heightPaddle diameterProduct densityProduct flowabilityCohesionParticle sizeLiquid additionRequired uniformity

Do not size the mixer from gross vessel volume alone.

04Topic

Rapid Mixing Without Uncontrolled Shear

Fluidized-zone mixers are known for short batch cycles, but rapid mixing does not automatically mean high shear.

In the fluidized zone, particles can move with reduced bulk friction because they are temporarily separated rather than continuously compressed against one another.

PerMix legacy literature identifies typical mixing times of approximately 30–60 seconds for many free-flowing products and describes the action as low-friction and suitable for selected fragile or heat-sensitive products. These values should be treated as application examples—not universal guarantees.

Other commercial fluidized-zone systems also report cycle times ranging from seconds to a few minutes, depending on product and process.

Actual Cycle Time Depends On

Product flowabilityBulk densityParticle sizeDensity differencesMinor-ingredient concentrationPaddle geometryShaft speedWorking fillLiquid additionRequired uniformitySampling method

05Topic

Gentle Handling of Fragile Products

A properly configured fluidized-zone mixer can be surprisingly gentle despite its rapid batch circulation.

Potential applications can include:

FlakesSpray-dried powdersAgglomerated beverage powdersGranulesPelletsCrystalsFragile food ingredientsCoated particles

The mechanically fluidized zone can reduce the amount of time particles spend compacted against the vessel or dragged through a dense powder bed.

However, product damage still depends on:

Paddle tip speedPaddle profileProduct drop pathMixing timeParticle strengthFill levelChopper useLiquid additionDischarge method

Preliminary Selection Direction

Choose a fluidized-zone mixer when:

Rapid mixing and particle protection are both importantThe product can tolerate controlled paddle contactDensity or particle-size variation must be overcomeShort residence time reduces total mechanical exposure

Choose a conventional paddle mixer when:

Gentleness is more important than maximum cycle speed

Choose a double cone mixer when:

The material is highly free-flowing and requires the lowest practical mechanical input

06Topic

Mixing Ingredients with Different Densities

Fluidized-zone mixers are frequently selected for formulations containing ingredients with differences in:

Bulk densityParticle sizeParticle shapeConcentrationSurface behavior

The central mechanically fluidized region allows particles to exchange position rapidly rather than remaining locked in a densely packed bed.

Potential applications include:

Vitamin premixesMineral premixesFeed additivesProtein blendsBeverage powdersDetergentsConstruction additivesPolymer compoundsBattery powdersChemical premixes

Important Limitation

The mixer can help create uniformity inside the vessel.

It cannot prevent segregation created later by:

Free fallPneumatic conveyingScrew conveyingVibrationSurge storagePackagingTransportation

Discharge and downstream handling must be evaluated with the mixer.

07Topic

Minor-Ingredient Distribution

Fluidized-zone mixers can be effective for low-percentage ingredients because the batch is repeatedly separated and recombined through overlapping active zones.

Potential minor ingredients include:

VitaminsMineralsFlavorsColorsEnzymesCatalystsConductive additivesStabilizersAnti-caking agentsFunctional additivesProcessing aids

Performance depends on:

Inclusion percentagePreblend strategyAddition pointLoading sequenceParticle sizeBulk densityCohesionElectrostatic behaviorBatch fillMixing timeSampling methodDischarge

For extremely low inclusion levels, preblending or staged addition may still be required.

08Topic

Liquid Addition and Powder Coating

The Fluidized Zone Creates a Strong Spray-Exposure Region

Liquid addition is one of the strongest potential applications for fluidized-zone mixing.

The paddles continually separate and expose powder particles, creating a moving surface for the spray system.

Potential liquids can include:

OilsFatsFlavorsBindersWaterSyrupsLecithinSurfactantsFragrancesColor solutionsFunctional coatingsDust suppressantsSolventsProcessing aids

Commercial fluidized-zone mixers use the highly mobile central particle region to expose substantial powder surface area to liquid sprays.

Liquid-System Engineering Variables

Total addition percentageLiquid viscosityLiquid temperatureAddition rateNozzle typeDroplet sizeSpray angleNozzle positionNumber of nozzlesPowder absorbencyProduct temperatureAgglomeration tendencyRequired coating uniformityFinal flowabilityCleaning method

Potential Liquid Systems

Metering pumpHeated liquid tankHeated delivery lineFlow meterPressure controlAir-atomizing nozzlesHydraulic nozzlesMultiple spray zonesStaged additionRecipe controlJacketed dosing skid

09Topic

Flow-Distortion Tools and Choppers

Use Localized Energy Where the Process Requires It

The primary paddles create total-batch circulation.

Optional high-speed tools can provide additional localized energy for:

Breaking soft lumpsDistributing difficult liquidsReducing wet agglomeratesImproving coatingControlling particle growthDispersing low-percentage additives

Potential tools can include:

High-speed choppersPin barsFlow-distortion toolsIntensive side toolsApplication-specific cutters

A Chopper Should Not Correct Poor Paddle Circulation

The complete batch must pass through the chopper’s active zone.

If the primary paddle system does not circulate the material correctly, the chopper may repeatedly work only a small region of the batch.

Chopper Engineering Variables

Tool diameterTool profileTip speedPositionQuantityShaft sealBearing arrangementProduct residence through the active zoneAgglomerate strengthProduct fragilityLiquid-addition sequenceWearCleaning

10Topic

Agglomeration and Instantization

A fluidized-zone mixer can support selected particle-enlargement processes when a liquid binder is distributed through the mobile powder bed.

Potential objectives can include:

Controlled agglomerationInstantizationImproved wettabilityReduced dustImproved flowabilitySurface coatingIncreased bulk densityImproved product appearance

The process may include:

Dry premixingBinder preparationControlled spray additionNucleationParticle growthChopper or tool controlEndpoint determinationDischargeDownstream drying or cooling

Important Limitation

A fluidized-zone mixer is not automatically a substitute for a dedicated high-shear granulator or continuous agglomeration system.

The correct equipment depends on:

Required particle sizeGranule strengthPorosityLiquid percentageBinder chemistryDrying methodProduct residence timeThroughput

Mixer comparison

Is a Fluidized-Zone Mixer the Right Choice?

When to Choose a QuantumX Fluidized-Zone Mixer

Choose this platform when:

  • Very short batch cycles are important
  • High production throughput is required
  • Ingredients differ in particle size or bulk density
  • Low-percentage additives must distribute rapidly
  • Product must be mixed quickly without excessive heat
  • Selected fragile particles must remain intact
  • Liquid must be sprayed uniformly
  • Surface coating is required
  • Rapid full-length discharge is valuable
  • Downstream segregation must be minimized through fast emptying
  • A twin-shaft system fits the plant layout
  • The process may require sanitary, ATEX, vacuum or containment engineering

When It May Not Be the Best Choice

Another platform may be more appropriate when:

  • The product is a heavy paste
  • Extremely high viscosity is involved
  • Hard agglomerates require milling
  • The material is highly adhesive
  • Very aggressive wet granulation is required
  • The process needs continuous rather than batch mixing
  • Maximum gentleness is more important than cycle time
  • The plant cannot accommodate the drive and maintenance access
  • The batch size is too small to establish the intended fluidized zone
  • The product becomes non-flowing after liquid addition
  • A pressure-rated reactor is the primary process requirement
  • The desired process is primarily drying rather than mixing

Potential alternatives include:

  • Standard Paddle Mixer
  • Ribbon Mixer
  • Ploughshare Mixer
  • Double Cone Mixer
  • Conical Screw Mixer
  • Sigma Mixer
  • Double Planetary Mixer
  • Multi-Shaft Mixer
  • EmulXion liquid-processing system

Fluidized-Zone Mixer vs. Conventional Paddle Mixer

A fluidized-zone mixer is a specialized paddle architecture, but it should not be treated as identical to every conventional paddle mixer.

RequirementQuantumX Fluidized-Zone MixerStandard Paddle Mixer
Shaft arrangementUsually twin counter-rotating shaftsCommonly one shaft; horizontal or vertical
Vessel geometryW-shaped or twin troughSingle trough or vertical vessel
Primary actionOverlapping mechanically fluidized zonesControlled lifting and folding
Mixing speedVery rapid for suitable formulationsModerate and controlled
Product intensityRapid exchange with low-to-moderate shearGentler overall
Density differencesStrong capabilityStrong for many formulations
Fragile particlesStrong when properly configuredOften preferred for maximum gentleness
Liquid additionStrong spray exposureControlled moderate addition
DeagglomerationChoppers or intensive tools availableChoppers available where required
DischargeFull-length bomb-bay optionsCenter, full-length or bomb-bay
Working fillMust preserve fluidization headspaceApplication-specific
Mechanical complexityTwo shafts and synchronized driveOften simpler
Best selection driverCycle time and rapid particle exchangeProduct integrity and gentle control

Fluidized-Zone Mixer vs. Ribbon Mixer

RequirementFluidized-Zone MixerRibbon Mixer
Primary actionMechanically fluidized particle exchangeOpposing axial and radial circulation
Typical cycleVery short for suitable productsModerate
General dry blendingExcellentExcellent
Density differencesStrongStrong
Minor ingredientsStrongStrong
Fragile materialsStrong when properly configuredApplication-dependent
Liquid additionStrongModerate
Working fill flexibilityRequires fluidization headspaceRequires ribbon engagement
Drive complexityTwin synchronized shaftsSingle shaft in common configuration
DischargeRapid full-length doorsCenter or full-length options
CleaningTwo shafts and paddlesRibbons, supports and shaft
Best selection driverHigh throughput and short cyclesFlexible general-purpose blending

Fluidized-Zone Mixer vs. Plough Mixer

RequirementFluidized-Zone MixerPlough Mixer
Primary actionTwin-shaft mechanically fluidized zoneHigh-intensity plough fluidization
Product intensityRapid but potentially gentleMore intensive
Fragile particlesOften strongerApplication-dependent
Cohesive powdersApplication-dependentOften stronger
Liquid additionStrongVery strong
DeagglomerationOptional choppersStrong primary action plus choppers
GranulationSelected applicationsStronger pathway
Heat generationGenerally lower for suitable productsPotentially higher
WearApplication-dependentPotentially higher
Best selection driverSpeed, uniformity and product protectionCohesion, coating and deagglomeration

QuantumX configurations

01Configuration

Rapid Full-Length Discharge

Empty the Batch Before a New Segregation Mechanism Develops

A major advantage of twin-shaft fluidized-zone mixers can be rapid discharge through full-length bomb-bay or drop-bottom doors.

Potential benefits include:

Shorter total cycleReduced residual heelLess time for segregationReduced manual cleanoutDirect discharge into a surge hopperFast transfer to packagingImproved production throughput

PerMix legacy documentation describes large bomb-bay doors for rapid emptying and reduced segregation after mixing.

Discharge Engineering Variables

Number of doorsDoor widthDoor sealActuationOpening sequencePosition confirmationVessel reinforcementDust containmentDownstream hopper volumeProduct flowabilityProduct fragilityRequired discharge timeSafety interlocks

Potential Discharge Systems

Full-length bomb-bay doorsTwin drop-bottom doorsCenter dischargeMultiple flush valvesContained dischargeDirect surge hopperPackaging-system connectionPneumatic transferScrew-conveyor connection

02Configuration

Heating and Cooling

Thermal Control Is Possible—but Duty Must Be Calculated

Fluidized-zone mixers can include heating or cooling jackets when product temperature affects:

FlowabilityCoatingBinder viscosityProduct stabilityDownstream processingDryingCoolingReaction rate

The mechanically active product movement can renew contact with the vessel wall.

However, the short mixing cycles associated with fluidized-zone systems do not automatically provide enough residence time for a major thermal duty.

Thermal performance depends on:

Jacket areaProduct-contact areaProduct thermal propertiesBatch massShaft speedWall renewalThermal mediumThermal-medium flowVessel-wall thicknessRequired temperature changeAvailable process time

Standard Thermal Options

Low-pressure hot-water jacketCooling-water jacketGlycol jacketInsulationStainless-steel claddingProduct-temperature sensorsBasic temperature controls

QuantumX Thermal Options

Move into a fully engineered QuantumX thermal system when the application requires:

SteamThermal oilVacuumPressureSolvent removalCondensationControlled dryingAdvanced endpoint controlASME or PED construction

03Configuration

Vacuum Fluidized-Zone Mixers

A QuantumX fluidized-zone system can be evaluated for vacuum when the process requires:

Oxygen reductionClosed powder processingVacuum deaerationMoisture removalSolvent removalControlled atmosphereReduced product exposureCondensation and recovery

Vacuum changes the complete mechanical and process design.

The review must include:

Vessel external-pressure designShaft sealsDoor sealsAccess openingsFilter systemVapor loadProduct expansionDust carryoverVacuum pumpCondenserReceiverShaft-speed effectProduct behavior under reduced pressure

Important Selection Note

A fluidized-zone mixer is optimized first for rapid mixing.

If vacuum drying is the dominant process objective, QuantumX may recommend:

Ribbon mixer-dryerPaddle mixer-dryerPlough mixer-dryerConical screw mixer-dryerDouble cone vacuum dryer

The correct platform depends on moisture or solvent load, drying time, product fragility and thermal duty.

04Configuration

Pressure-Rated and ASME Fluidized-Zone Systems

Selected QuantumX fluidized-zone systems can be engineered for:

Positive internal pressureVacuum-and-pressure cyclesGas treatmentInert-gas operationASME constructionPED compliancePressure-rated jacketsControlled reaction or coating

A pressure-rated twin-shaft mixer must account for:

Vessel shell and headsTwin shaft penetrationsMultiple shaft sealsChopper penetrationsDrop-bottom door designAccess-door designJacket interactionDynamic agitator loadsSupport loadsPressure cyclesThermal cyclesRelief interfaces

A standard bomb-bay discharge may not be compatible with every pressure requirement.

The complete vessel, closure and discharge strategy must be engineered together.

05Configuration

ATEX and Hazardous-Area Fluidized-Zone Mixers

QuantumX can engineer fluidized-zone systems around defined:

Dust zonesGas or vapor zonesInternal and external classificationsEquipment categoriesGas or dust groupsTemperature classesMaximum surface temperaturesMechanical ignition risksStatic-control requirementsNitrogen inertingOxygen monitoringExplosion-protection interfaces

Fluidized-zone mixers require careful review of:

Two shaft systemsMultiple bearingsMultiple shaft sealsPaddle clearancesShaft synchronizationChopper toolsBearing temperaturesProduct temperaturesStatic generationForeign-body riskDrop-bottom doors

Potential Safeguards

ATEX-rated motors and instrumentsGrounding and bondingConductive componentsBearing-temperature monitoringShaft-speed monitoringSynchronization monitoringSeal-purge monitoringProduct-temperature monitoringMotor-current monitoringTorque monitoringVibration monitoringNitrogen purgeOxygen monitoringSafe opening interlocksExplosion-protection interfaces

06Configuration

High-Containment Fluidized-Zone Mixers

Fluidized-zone systems can be integrated into contained powder-processing lines.

Potential containment features include:

Closed chargingContained bag dumpingVacuum conveyingSplit-butterfly valvesGlovebox interfacesHigh-integrity shaft sealsFiltered ventingClosed samplingContained dischargeEnclosed bomb-bay receiverWash-in-placeClean-in-placeNitrogen inertingOxygen monitoring

Potential applications include:

Potent pharmaceutical powdersSensitizing materialsToxic chemicalsNanomaterialsCarbon blackCarbon nanotubesBattery materialsHigh-value catalystsDusty fine powders

The containment target and test basis must be defined before final design.

07Configuration

Sanitary and Easy-Clean Design

QuantumX sanitary fluidized-zone mixers can include:

304, 316 or 316L stainless steelDefined internal surface finishContinuous product-contact weldsGround and polished transitionsElectropolishingPassivationLarge access doorsReduced product trapsSanitary spray nozzlesCleanable shaft sealsRetractable or removable shaft arrangementsRemovable paddles where appropriateCIP spray devicesWash-in-place systemsDrainable geometryFlush discharge sealsStainless-steel exterior claddingBatch traceabilityRecipe control

PerMix legacy literature describes access-door, retractable-drive and CIP spray-ball options for its fluidized-zone mixer platform.

08Configuration

Retractable Shafts and Drive Assemblies

For applications requiring frequent inspection or deep cleaning, a retractable shaft or drive system may be evaluated.

Potential benefits include:

Improved access to trough surfacesEasier paddle inspectionBetter seal accessReduced cleaning obstructionFaster maintenanceImproved changeover

Engineering considerations include:

Structural supportAlignmentRail or withdrawal mechanismSeal reconnectionShaft synchronizationElectrical reconnectionGuardingMaintenance spaceFloor loadingRepeatable reassemblyClearance verification

A retractable system requires additional plant space and should be included in the layout from the beginning.

Materials of Construction

Materials of Construction

Carbon Steel

Can be evaluated for:

  • Construction materials
  • Minerals
  • Fertilizers
  • General industrial powders
  • Non-corrosive chemical blends
304 Stainless Steel

Can be evaluated for:

  • Food ingredients
  • General sanitary products
  • Moderate-corrosion applications
  • Animal nutrition
  • Cleanable industrial powders
316 and 316L Stainless Steel

Can be evaluated for:

  • Pharmaceuticals
  • Nutraceuticals
  • Specialty chemicals
  • Salt-containing formulations
  • High-purity materials
  • Aggressive cleaning environments
Duplex and Specialty Stainless Steels

Can be considered where standard stainless grades do not provide the required corrosion resistance or mechanical performance.

Hastelloy and Nickel Alloys

Can be evaluated for:

  • Corrosive chemicals
  • Solvent service
  • Reactive intermediates
  • High-purity products
  • Aggressive cleaning

The vessel, paddles, shafts, fasteners, seals, choppers and discharge components must be reviewed together.

Titanium

Can be evaluated for selected:

  • Chloride-sensitive processes
  • Corrosive intermediates
  • High-purity formulations
  • Metal-sensitive applications

The design must account for:

  • Titanium grade
  • Welding
  • Shaft stiffness
  • Paddle stiffness
  • Galling
  • Dissimilar-metal contact
  • Fatigue
  • Thermal expansion
  • Repair strategy
Abrasion-Resistant Construction

Abrasive materials can wear:

  • Paddle leading edges
  • Paddle faces
  • Trough walls
  • Choppers
  • Spray nozzles
  • Drop-bottom doors
  • Door seals
  • Discharge transitions

Potential protection includes:

  • Hardox vessel sections
  • Replaceable wear liners
  • Hardened paddle edges
  • Tungsten-carbide coatings
  • Ceramic liners
  • Ceramic inserts
  • Wear-resistant chopper tools
  • Protected discharge doors
  • Replaceable high-wear components

Legacy PerMix literature identifies tungsten-carbide-coated paddle edges as an option for abrasive fluidized-zone applications.

Ceramic-Lined Fluidized-Zone Mixers

Ceramic lining can be evaluated for:

  • High-purity powders
  • Abrasive products
  • Reduced metallic contamination
  • Battery materials
  • Electronic ceramics
  • Catalysts
  • Pigments
  • Specialty minerals

A ceramic-lined twin-shaft mixer must be designed around:

  • Liner type
  • Liner thickness
  • Attachment method
  • Impact
  • Paddle-to-liner clearance
  • Shaft deflection
  • Thermal expansion
  • Chopper interaction
  • Door transitions
  • Door sealing
  • Product traps
  • Replaceability
  • Added weight
  • Static behavior

The close interaction of twin shafts and trough surfaces makes liner tolerance especially important.

A ceramic liner should not be added to a standard-clearance design after the mixer geometry has been established.

Technical details

Controls, Integration and Testing

Controls and Instrumentation

Potential QuantumX controls can include:

  • PLC and HMI
  • Shaft-speed control
  • Shaft synchronization
  • Phase monitoring
  • Recipe management
  • Batch timers
  • Load-cell weighing
  • Ingredient sequencing
  • Liquid-dosing control
  • Nozzle pressure monitoring
  • Chopper control
  • Product-temperature monitoring
  • Jacket control
  • Motor-current monitoring
  • Torque monitoring
  • Bearing-temperature monitoring
  • Seal-purge monitoring
  • Vibration monitoring
  • Door-position confirmation
  • Vacuum control
  • Pressure monitoring
  • Nitrogen inerting
  • Oxygen monitoring
  • Alarm history
  • Batch reporting
  • User access levels
  • Data logging
  • Remote support

Safety Interlocks Can Include

  • Mixer cannot operate with an access door open
  • Mixer cannot operate with discharge doors open
  • Discharge cannot open during the mixing cycle
  • Choppers cannot operate outside the approved sequence
  • Mixer shuts down on loss of shaft synchronization
  • Mixer shuts down on high bearing temperature
  • Mixer shuts down on excessive torque
  • Mixer shuts down on high product temperature
  • Vacuum or pressure cycles require confirmed closures
  • Safe opening requires zero speed and pressure equalization
Loading and Ingredient Handling

QuantumX fluidized-zone mixers can integrate with:

  • Bag-dump stations
  • Bulk-bag unloaders
  • Silos
  • Day bins
  • Loss-in-weight feeders
  • Gain-in-weight systems
  • Screw feeders
  • Pneumatic conveying
  • Vacuum conveying
  • Minor-ingredient dosing
  • Microingredient systems
  • Liquid-dosing skids
  • Binder-preparation systems
  • Gas addition
  • Dust collection

Loading Sequence Matters

The order of addition may affect:

  • Minor-ingredient distribution
  • Fragile-particle damage
  • Agglomeration
  • Liquid exposure
  • Mixing time
  • Product temperature
  • Discharge

The control system can manage staged charging based on:

  • Weight
  • Time
  • Ingredient confirmation
  • Feeder status
  • Mixer status
  • Shaft speed
  • Liquid-addition stage
Downstream Integration

Rapid mixing only creates high throughput when downstream equipment can accept the batch.

The mixer can connect to:

  • Surge hopper
  • Screw conveyor
  • Pneumatic conveying
  • Vacuum transfer
  • Screening
  • Sifting
  • Milling
  • Metal detection
  • Cooling
  • Drying
  • Agglomeration
  • Bagging
  • Filling
  • Packaging
  • Checkweighing

The downstream surge volume should be large enough to accept the full rapid-discharge batch.

Otherwise, the mixer may wait for the downstream process and lose the throughput benefit of the short mixing cycle.

Batch Throughput Is More Than Mixing Time

Total production cycle includes:

  • Ingredient preparation
  • Charging
  • Mixer loading
  • Dry premixing
  • Liquid addition
  • Final mixing
  • Discharge
  • Downstream acceptance
  • Cleaning
  • Recipe changeover

A 30-second mixing time does not create a 30-second production cycle.

QuantumX evaluates the complete cycle to identify the actual production bottleneck.

Throughput Calculation

Total cycle time = Loading time + Mixing time + Liquid-addition time + Discharge time + Waiting time + Cleaning or changeover allowance

Batches per hour = 60 minutes ÷ Total cycle time in minutes

Hourly throughput = Batch mass × Batches per hour

Testing and Factory Acceptance

Define Uniformity Before Testing the Mixer

Potential FAT activities include:

  • Mechanical inspection
  • Shaft rotation
  • Shaft synchronization
  • Speed range
  • Motor current
  • Torque monitoring
  • Bearing-temperature monitoring
  • Access-door interlocks
  • Discharge-door operation
  • Door-seal inspection
  • Load-cell verification
  • Ingredient sequencing
  • Liquid-dosing operation
  • Spray-nozzle operation
  • Chopper operation
  • Jacket function
  • Vacuum function
  • Nitrogen purge
  • Oxygen monitoring
  • Alarm simulation
  • Batch reporting
  • Cleaning access
  • Product trial when agreed

Product-Test Protocol

A product-test protocol should define:

  • Test quantity
  • Product identity
  • Ingredient concentrations
  • Loading sequence
  • Shaft speed
  • Mixing time
  • Liquid-addition rate
  • Sampling locations
  • Number of samples
  • Analytical method
  • Uniformity target
  • Particle-damage limit
  • Product-temperature limit
  • Discharge time
  • Residual hold-up method
  • Cleaning procedure

Industries and applications

Industries and Applications

PerMix’s earlier fluidized-zone literature identifies applications including building materials, fly ash conditioning, animal feeds, mineral premixes, instant drinks, milk powders and vitamin mixes.

Why QuantumX

Why Manufacturers Choose QuantumX Fluidized-Zone Mixers

  • 01

    Rapid Particle Exchange

    Overlapping paddle trajectories create rapid movement through the complete batch.

  • 02

    Short Batch Cycles

    Suitable formulations can reach the required blend uniformity substantially faster than conventional low-intensity mixers.

  • 03

    Product Protection

    The mechanically fluidized zone can provide rapid mixing with limited total exposure time and reduced bulk friction.

  • 04

    Strong Liquid Distribution

    The mobile powder bed continually exposes fresh surface to spray nozzles.

  • 05

    Fast Discharge

    Full-length drop-bottom doors can empty the batch rapidly and reduce post-mix segregation.

  • 06

    Single- and Twin-Shaft Options

    The platform can be configured around the required batch size, intensity, complexity and investment level.

  • 07

    Specialty Construction

    Available engineering pathways can include stainless steel, Hastelloy, titanium, ceramic lining and wear-resistant systems.

  • 08

    QuantumX Compliance Pathways

    Vacuum, pressure, ASME, PED, ATEX, inerting and high containment can be integrated where required.

  • 09

    Complete Process Systems

    QuantumX can coordinate:

    FeedingWeighingLiquid dosingVacuumThermal controlInertingDischargeScreeningPackagingControlsDocumentation

APPLICATION ENGINEERING BEFORE EQUIPMENT SELECTION

Fluidized-Zone Mixer Design Information

Tell Us What Must Mix—and How Quickly It Must Be Discharged

Provide:

  1. Product or formulation
  2. Batch mass
  3. Loose bulk density
  4. Operating bulk density
  5. Minimum batch size
  6. Maximum batch size
  7. Particle size
  8. Particle-size distribution
  9. Particle shape
  10. Flowability
  11. Cohesiveness
  12. Agglomerate strength
  13. Fragility
  14. Abrasion
  15. Corrosion
  16. Minor-ingredient percentage
  17. Required blend uniformity
  18. Current mixing time
  19. Required mixing time
  20. Liquid-addition percentage
  21. Liquid viscosity
  22. Liquid temperature
  23. Required coating result
  24. Deagglomeration requirement
  25. Agglomeration requirement
  26. Product-temperature limit
  27. Heating requirement
  28. Cooling requirement
  29. Vacuum requirement
  30. Operating pressure
  31. Design pressure
  32. Inert-gas requirement
  33. Oxygen target
  34. Hazardous-area classification
  35. Containment target
  36. Materials of construction
  37. Surface finish
  38. Wear-protection requirement
  39. Liner requirement
  40. Cleaning method
  41. CIP requirement
  42. Loading method
  43. Ingredient sequence
  44. Sampling method
  45. Discharge method
  46. Required discharge time
  47. Residual hold-up target
  48. Upstream equipment
  49. Downstream equipment
  50. Required hourly throughput
  51. Available footprint
  52. Available headroom
  53. Utilities and voltage
  54. Documentation requirements

Upload material data sheets, safety data sheets, batch requirements, bulk-density data, particle information, liquid-addition requirements, uniformity criteria, hazardous-area information or facility drawings. Confirm an approved confidential communication channel before submitting proprietary formulas.

john.paul@procxinc.com

Frequently asked questions

Frequently Asked Questions

Got more questions?Ask an engineer
What is a fluidized-zone mixer?

A fluidized-zone mixer uses mechanically driven paddles to lift, separate and rapidly exchange powder particles inside a controlled active mixing region.

Is a fluidized-zone mixer the same as a fluid-bed dryer?

No. A fluidized-zone mixer creates the principal mixing action mechanically. A fluid-bed dryer normally uses process air to suspend, dry or cool particles.

Is it the same as a twin-shaft paddle mixer?

A twin-shaft fluidized-zone mixer is a specialized paddle-mixer configuration using two counter-rotating shafts and overlapping active zones.

Is it also called a non-gravity or zero-gravity mixer?

Those terms are used in the market, although the material does not become literally weightless. The process creates a mechanically mobilized, lower-density particle zone.

How does a twin-shaft fluidized-zone mixer work?

Counter-rotating paddles sweep the lower W-shaped troughs and lift material toward the central region between the shafts, where particles exchange position rapidly.

Is a single-shaft version available?

Single-shaft configurations can be evaluated for suitable products and less demanding mixing duties.

When is a twin-shaft version preferred?

Twin shafts are generally preferred for larger batches, short cycle requirements, significant density differences, demanding liquid addition and high throughput.

How fast does it mix?

Some suitable free-flowing formulations can reach the required uniformity in tens of seconds. Final cycle time depends on the product, mixer geometry, fill level, liquid addition and analytical target.

Can it mix products with different densities?

Yes, potentially. The fluidized zone can support rapid exchange of ingredients with different densities, particle sizes and shapes. Final performance must still be validated.

Is it suitable for fragile materials?

It can be, when paddle geometry, speed and cycle time are selected appropriately. Extremely fragile materials may be better suited to a conventional paddle or double cone mixer.

Is it low shear?

The fluidized-zone action can provide rapid mixing with relatively low bulk friction, but actual shear depends on shaft speed, paddle geometry, product and optional choppers.

Can liquids be added?

Yes. Liquid addition and particle coating are important potential applications.

Where should spray nozzles be positioned?

Nozzles should be positioned so the spray enters an active, well-exposed product region. Final location depends on vessel geometry, liquid properties and powder behavior.

Can it coat particles or pellets?

Yes, for suitable formulations. Coating performance depends on spray quality, liquid rate, product circulation, particle strength and final flowability.

Can it agglomerate powders?

Selected agglomeration and instantization duties can be evaluated. Applications requiring strong granule growth may require a dedicated granulation system.

Can choppers be added?

Yes. High-speed choppers or intensive tools can be added for soft-lump breakup, liquid distribution and agglomerate control.

Can it break hard lumps?

A mixer is not a substitute for a mill. Hard agglomerates may require upstream delumping or milling.

Why use full-length bomb-bay doors?

Large bottom doors can provide rapid discharge, reduce residual hold-up and reduce the time available for post-mix segregation.

Can it be heated or cooled?

Yes. Jacketed systems can be evaluated, but the thermal duty and available process time must be calculated.

Can it operate under vacuum?

Selected QuantumX systems can be engineered for vacuum. If drying is the primary duty, another QuantumX mixer-dryer configuration may be more appropriate.

Can it operate under positive pressure?

Selected pressure-rated systems can be engineered under QuantumX. The vessel, twin shaft seals, choppers, doors and jacket must be reviewed together.

Can it be ASME or PED rated?

Application-specific ASME or PED systems can be evaluated.

Are ATEX versions available?

QuantumX can engineer fluidized-zone mixers around defined ATEX or hazardous-area requirements supplied by the customer.

Can it be nitrogen inerted?

Yes. Systems can include nitrogen purge, oxygen monitoring, pressure control and process interlocks.

Can it provide high containment?

Closed charging, filtered venting, high-integrity seals, contained sampling and enclosed discharge can be integrated.

Are sanitary versions available?

Yes. Sanitary options can include 316L stainless steel, polished welds, access doors, cleanable seals, CIP devices and retractable shaft arrangements.

Can the shafts be removed for cleaning?

Retractable or removable shaft and drive arrangements can be evaluated for appropriate models and plant layouts.

Can it be ceramic lined?

Yes, for suitable applications. Liner thickness, tolerances, paddle clearances, door transitions and static behavior must be incorporated into the original design.

Are Hastelloy and titanium available?

Selected Hastelloy, nickel-alloy and titanium constructions can be evaluated for suitable corrosive or high-purity applications.

How does it compare with a ribbon mixer?

The fluidized-zone mixer generally provides faster particle exchange and stronger liquid distribution. The ribbon mixer provides versatile convective blending with simpler single-shaft architecture.

How does it compare with a conventional paddle mixer?

A standard paddle mixer generally provides gentler lifting and folding. A twin-shaft fluidized-zone mixer is optimized for shorter cycles and rapid overlapping particle exchange.

How does it compare with a plough mixer?

A plough mixer generally applies more intensive mechanical action and is often stronger for highly cohesive materials, deagglomeration and granulation.

How is the correct size selected?

Sizing depends on batch mass, bulk density, working fill, particle behavior, liquid addition, cycle time, discharge time and hourly throughput.

Can QuantumX test my material?

Application testing can be evaluated when material quantity, hazards, confidentiality, test method and acceptance criteria are agreed.

What information is required for a quotation?

Provide the product, batch size, density, particle characteristics, uniformity target, liquid addition, cycle time, discharge requirement, construction, compliance and utilities.
QuantumX fluidized-zone mixers

Rapid Mixing. Controlled Fluidization. Engineered QuantumX Performance.

Choose a QuantumX fluidized-zone mixer when the process requires:

  • Rapid powder blending
  • Short batch cycles
  • High production throughput
  • Twin-shaft particle exchange
  • Ingredients with different densities
  • Minor-ingredient distribution
  • Gentle handling of selected fragile products
  • Liquid addition
  • Particle coating
  • Controlled agglomeration
  • Rapid full-length discharge
  • Sanitary construction
  • Wear-resistant construction
  • Ceramic lining
  • Vacuum
  • Pressure
  • ASME or PED
  • ATEX
  • Nitrogen inerting
  • High containment
  • Integrated feeding, controls and packaging

Request engineering support

Let’s talk about your process.

Share your material and batch requirements. A PerMix engineer will review the application and recommend a mixer.

+1 (855) PERMIXUSACall john.paul@procxinc.comEmail