A production line can appear fully utilized while losing capacity at its most critical step. A mixer may wait on upstream feeding, a dryer may be limited by poor heat transfer, or a reactor may require long hold times because dispersion is inconsistent. Process intensification addresses these constraints by redesigning how energy, materials, heat, mass transfer, and control are applied to the product.
For manufacturers, the objective is not simply to make a process smaller or faster. It is to produce more consistent material with less cycle time, less waste, lower energy use, and fewer opportunities for variation. That requires engineering the full process around actual material behavior, not adding equipment to an already inefficient sequence.
What Process Intensification Means in Manufacturing
Process intensification is the deliberate improvement of a manufacturing process by combining operations, increasing transfer rates, reducing unnecessary residence time, or applying more effective mechanical and thermal energy. In practical terms, it often means achieving the same production target with fewer steps, a smaller equipment footprint, or a substantially shorter batch cycle.
The concept applies across powders, liquids, slurries, pastes, emulsions, and high-viscosity formulations. A food producer may intensify liquid addition and dispersion inside a plough mixer rather than relying on a separate premix operation. A specialty chemical manufacturer may combine mixing, vacuum deaeration, heating, cooling, and reaction in one multi-functional vessel. A battery-material producer may improve powder coating quality by controlling shear, feed rate, and residence time in a continuous process.
The common factor is not a particular machine. It is a better use of process conditions.
Why Throughput Is Often Limited Outside the Mixer
Many capacity projects begin with the assumption that the existing mixer is undersized. Sometimes that is correct. More often, the true limitation sits at the interfaces surrounding the mixer: ingredient charging, liquid dosing, heating and cooling, vacuum pull-down, discharge, cleaning, or operator-dependent decisions.
A 30-minute mixing cycle is not truly a 30-minute cycle if charging requires 15 minutes, temperature control requires 20 minutes, and discharge takes another 10 minutes. Replacing the mixer with a larger model may increase batch size, but it may not improve output per shift as expected. The better question is: where does the material stop moving, changing, or reaching specification?
This is why process intensification begins with a process map. Engineers should measure the total batch timeline, identify the rate-limiting operation, and separate productive time from waiting time. Material properties must also be considered. A cohesive powder, shear-sensitive emulsion, or highly viscous paste will respond differently to increased speed, heat input, or vacuum.
Process Intensification Strategies That Deliver Results
The most effective approach depends on the material, required product quality, production volume, cleaning standard, and level of automation. Several strategies repeatedly produce measurable gains when they are properly matched to the application.
Combine Multiple Unit Operations
Combining steps inside a single engineered system can reduce transfers, handling losses, contamination risk, and cycle time. For example, a vacuum mixer can blend a viscous formulation, remove entrained air, support controlled heating or cooling, and prepare the material for direct discharge to filling or downstream processing.
In powder processing, a high-intensity mixer may blend ingredients, introduce liquid binders, agglomerate material, and begin drying under vacuum. Eliminating intermediate transfers can improve batch repeatability while reducing the floor space and labor required by separate equipment.
Integration is not automatically the right answer. A combined process can complicate maintenance, cleaning validation, and scheduling if one vessel becomes the sole path for several production operations. The value must be demonstrated through cycle-time analysis, quality improvement, and total operating cost, not assumed from a smaller equipment count.
Increase Mixing and Mass Transfer Efficiency
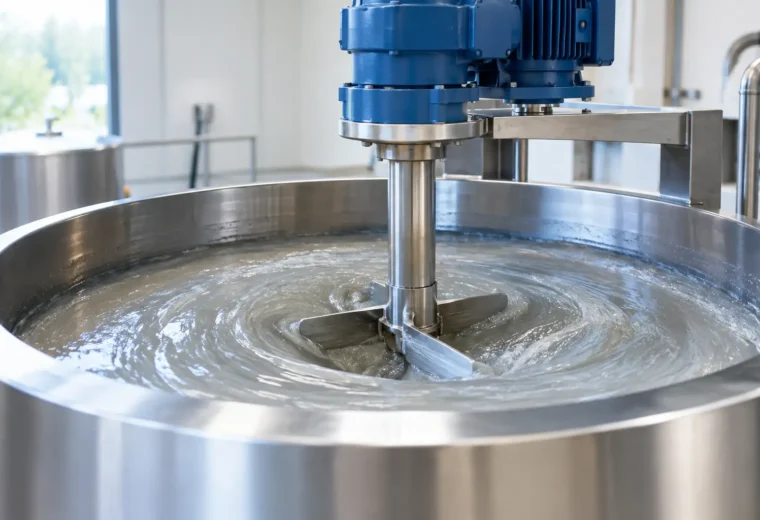
Mixing intensity should be selected based on what the material needs to achieve specification. Low-shear blending may be appropriate for fragile particles or free-flowing dry powders. High-shear dispersion may be necessary when breaking agglomerates, emulsifying immiscible liquids, wetting fine powders, or dispersing pigments and additives.
Improved mass transfer can shorten wet-out time, reduce the amount of liquid needed for processing, and prevent localized over-concentration. The design of agitators, choppers, rotor-stator devices, liquid injection points, and vessel geometry all influence the result. Adding power without improving the flow pattern can create hot spots, dead zones, excessive particle attrition, or unstable product behavior.
For high-viscosity applications, double planetary, multi-shaft, and sigma mixer configurations can bring material from the vessel wall and bottom into the active mixing zone. This is often more effective than attempting to force a conventional agitator to operate outside its practical viscosity range.
Improve Thermal Management
Heating and cooling are frequently the longest portions of a batch process. Intensification can involve increasing heat-transfer area, reducing product film thickness, improving wall scraping, or using agitation that renews contact between the material and the jacketed surface.
Thermal performance matters especially in reactions, crystallization, drying, melting, and high-viscosity mixing. Poor heat transfer does more than extend a batch. It can create temperature gradients that affect reaction selectivity, moisture content, viscosity, flavor, color, or particle structure.
Vacuum can also change thermal behavior. Lowering pressure can support low-temperature drying or deaeration, protecting heat-sensitive materials while reducing process time. However, vacuum capacity, condenser design, vapor load, and seal selection must be engineered together. A vacuum pump alone will not compensate for inadequate heat transfer or restricted vapor flow.
Move From Batch to Continuous Where It Fits
Continuous processing can intensify production by reducing inventory, stabilizing residence time, and allowing output to scale through run time rather than batch size. Continuous mixers are particularly effective for high-volume powder blending, dry ingredient incorporation, and applications requiring steady downstream feeding.
The trade-off is that continuous processing demands reliable feeding, accurate loss-in-weight control, and a clear understanding of start-up, shutdown, and material-traceability requirements. It may not be suitable for frequent formulation changes, very small campaign sizes, or processes that require extended reaction or maturation time. In those cases, a well-designed batch system may provide better flexibility and lower operational risk.
Engineering Process Intensification Around the Material
The best process design starts with the product rather than the equipment category. Particle size distribution, bulk density, flowability, moisture, viscosity curve, temperature sensitivity, shear sensitivity, and cleaning requirements determine which intensification methods are realistic.
A powder that bridges in a hopper can defeat an otherwise capable continuous mixer. A paste that changes viscosity during reaction may require torque reserve and a specialized agitator profile. An emulsion that meets specification in the laboratory may fail at production scale if shear exposure, recirculation volume, or heat removal changes.
This is why testing and scale-up are central to successful projects. Representative material trials should examine not only the final product sample but also the complete operating window. Engineers need to understand acceptable ranges for fill level, agitator speed, liquid addition rate, temperature, vacuum level, and discharge conditions. A process that performs only at one narrow setpoint is vulnerable to normal plant variation.
PerMix approaches these projects by evaluating mixing, feeding, thermal control, vacuum processing, discharge, and automation as connected decisions. The goal is measurable manufacturing performance, not a machine specification that looks favorable in isolation.
Automation Makes Gains Repeatable
Intensification creates value only when the improved process can be repeated shift after shift. Automation provides the control layer needed to maintain ingredient sequencing, dosing accuracy, mixing speed, temperature ramps, vacuum levels, and batch records.
For regulated and quality-sensitive production, automated recipe control can reduce operator variability and improve traceability. For higher-volume operations, it can shorten changeovers and allow the system to respond consistently to process signals. Sensors for torque, temperature, pressure, load cells, moisture, or particle characteristics can help operators identify deviations before they become rejected batches.
Automation should support the operation rather than add unnecessary complexity. The right level depends on production scale, product risk, available staffing, and maintenance capabilities. A straightforward semi-automated system can be more valuable than a complex control platform that plant personnel cannot efficiently maintain.
How to Evaluate a Process Intensification Project
A sound business case should compare the complete manufacturing impact, not only equipment purchase price. Useful measures include output per shift, batch cycle time, yield, utility consumption, labor hours, cleaning time, scrap rate, and maintenance exposure. Product-quality metrics should be equally prominent, including blend uniformity, particle integrity, viscosity, moisture, dispersion quality, and batch-to-batch consistency.
Before committing to capital equipment, define the current baseline and the required improvement. A target such as “increase capacity” is too broad. “Increase finished output from 8,000 to 12,000 pounds per shift while maintaining moisture variation within specification” gives engineering teams a design basis they can test.
The strongest projects address a real constraint, validate performance with the actual material, and account for the operational details that determine long-term reliability. When process intensification is treated as an engineering discipline rather than a speed-up exercise, it can turn the most limiting production step into a durable source of capacity, consistency, and cost control.